What are the considerations for selecting WP series worm gear reducers under strong impact and heavy load intermittent working conditions
1、 Key points of core parameter accountingTorque safety factor: It is necessary to distinguish between continuous operating torque and instantaneous peak impact. The rated output torque must be ≥ 2.0~2.5 times the actual maximum impact torque. In strong impact scenarios, the service factor is taken as 2.2~2.5, with an additional 10%~15% torque margin reserved.
Peak torque verification: The short-term peak torque allowed by the selected model must not be less than 1.5 times the rated torque, fully covering the instantaneous peak value of the impact load to prevent shaft and worm gear tooth surface fracture.
Thermal power verification: Intermittent impact under heavy load will accelerate heat accumulation, and it is necessary to ensure that the thermal balance power of the reducer is greater than or equal to the actual input power; If the natural heat dissipation limit is exceeded, it must be matched with forced air cooling or cooling coils.
2、 Requirements for Structure and Material Selection
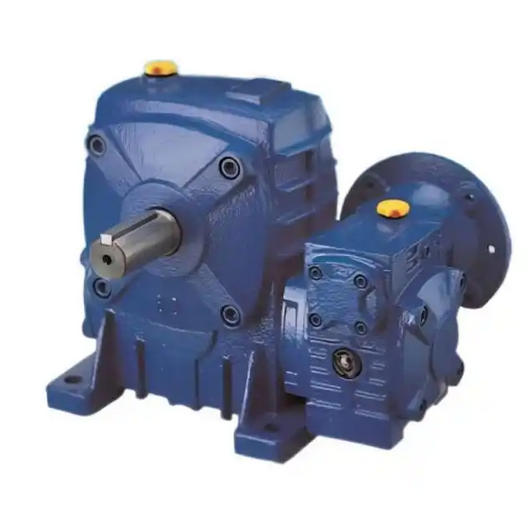
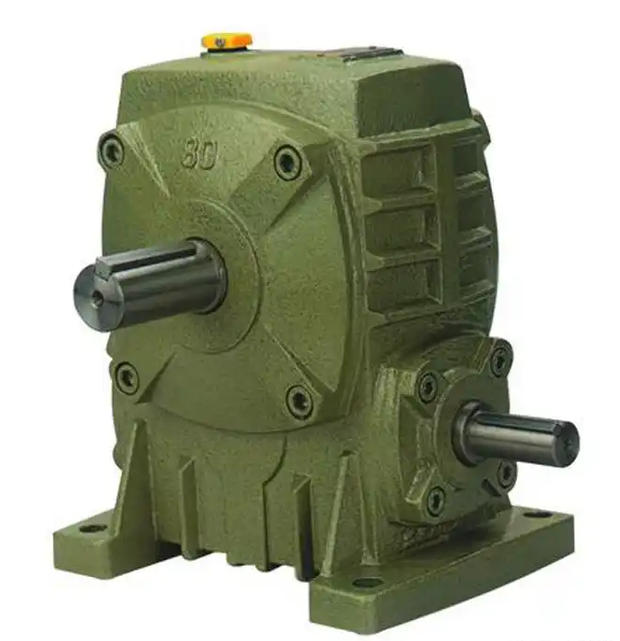
Prioritize the reinforced sub series: Avoid the basic universal WP/WPA and prioritize the WP hard tooth surface reinforced and WPX heavy-duty models. This type of worm gear has undergone 20CrMnTi carburizing and quenching treatment, with a tooth surface hardness of ≥ HRC58. The worm gear is made of ZCuSn10P1 high-strength tin bronze, which greatly improves its wear and impact resistance.
Box and bearing reinforcement: Select an integral thickened cast iron box, and require the supplier to provide a bearing rated dynamic load verification report to ensure that the radial and axial bearing capacity of the selected bearing fully covers the instantaneous force under impact load, avoiding shaft fracture caused by cantilever effect.
Installation structure adaptation: Priority should be given to horizontal foot installation to ensure sufficient lubrication; If vertical installation is required, it must be confirmed that the model is equipped with splash lubrication optimization or built-in oil pump to prevent dry grinding of the top of the worm gear due to oil shortage under heavy load impact.
3、 Key details of working condition adaptation
Self locking performance cannot replace braking: The WP series static self-locking may fail under strong impact and vibration conditions, and must be equipped with an external mechanical brake to prevent load reversal caused by impact loads, which may cause the worm gear tooth surface to crack.
Lubrication system upgrade: Under heavy load impact conditions, the use of ordinary industrial gear oil is prohibited. L-CKE/P 220 # extreme pressure type worm gear special oil must be selected. The first oil change should be made 200 hours in advance, and subsequent oil changes should be forced every 2000 hours to avoid dry friction caused by oil film rupture.
Strict control of input speed: The input speed of the worm gear must not exceed 1500r/min. It is recommended to control it within 1000r/min to reduce sliding friction heat generation and minimize damage to the meshing pair caused by impact loads.
4、 Selection of Avoid Pits Taboo
It is prohibited to select models with a safety factor of 1.2-1.5 times under normal stable working conditions, as rapid wear and shaft breakage of the worm gear are prone to occur under strong impact.
It is prohibited to use WP-E lightweight models with aluminum alloy shells. These models have insufficient box stiffness and are prone to box deformation and shaft misalignment under heavy load impact.
It is prohibited to select only the rated power of the motor and ignore the verification of peak impact torque and thermal power, otherwise problems such as sudden oil temperature rise and lubrication failure may occur.
Related News