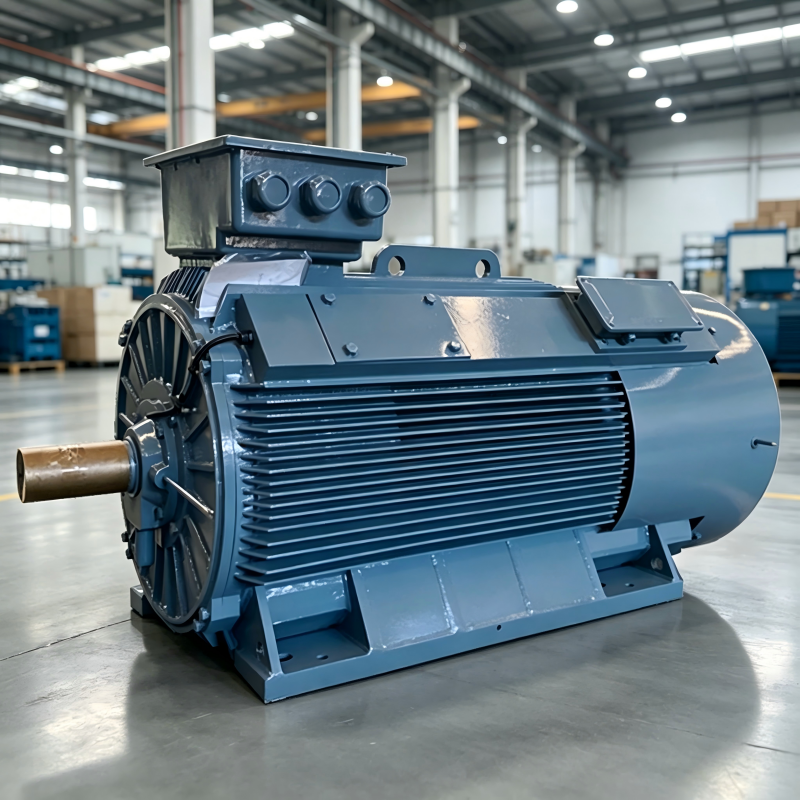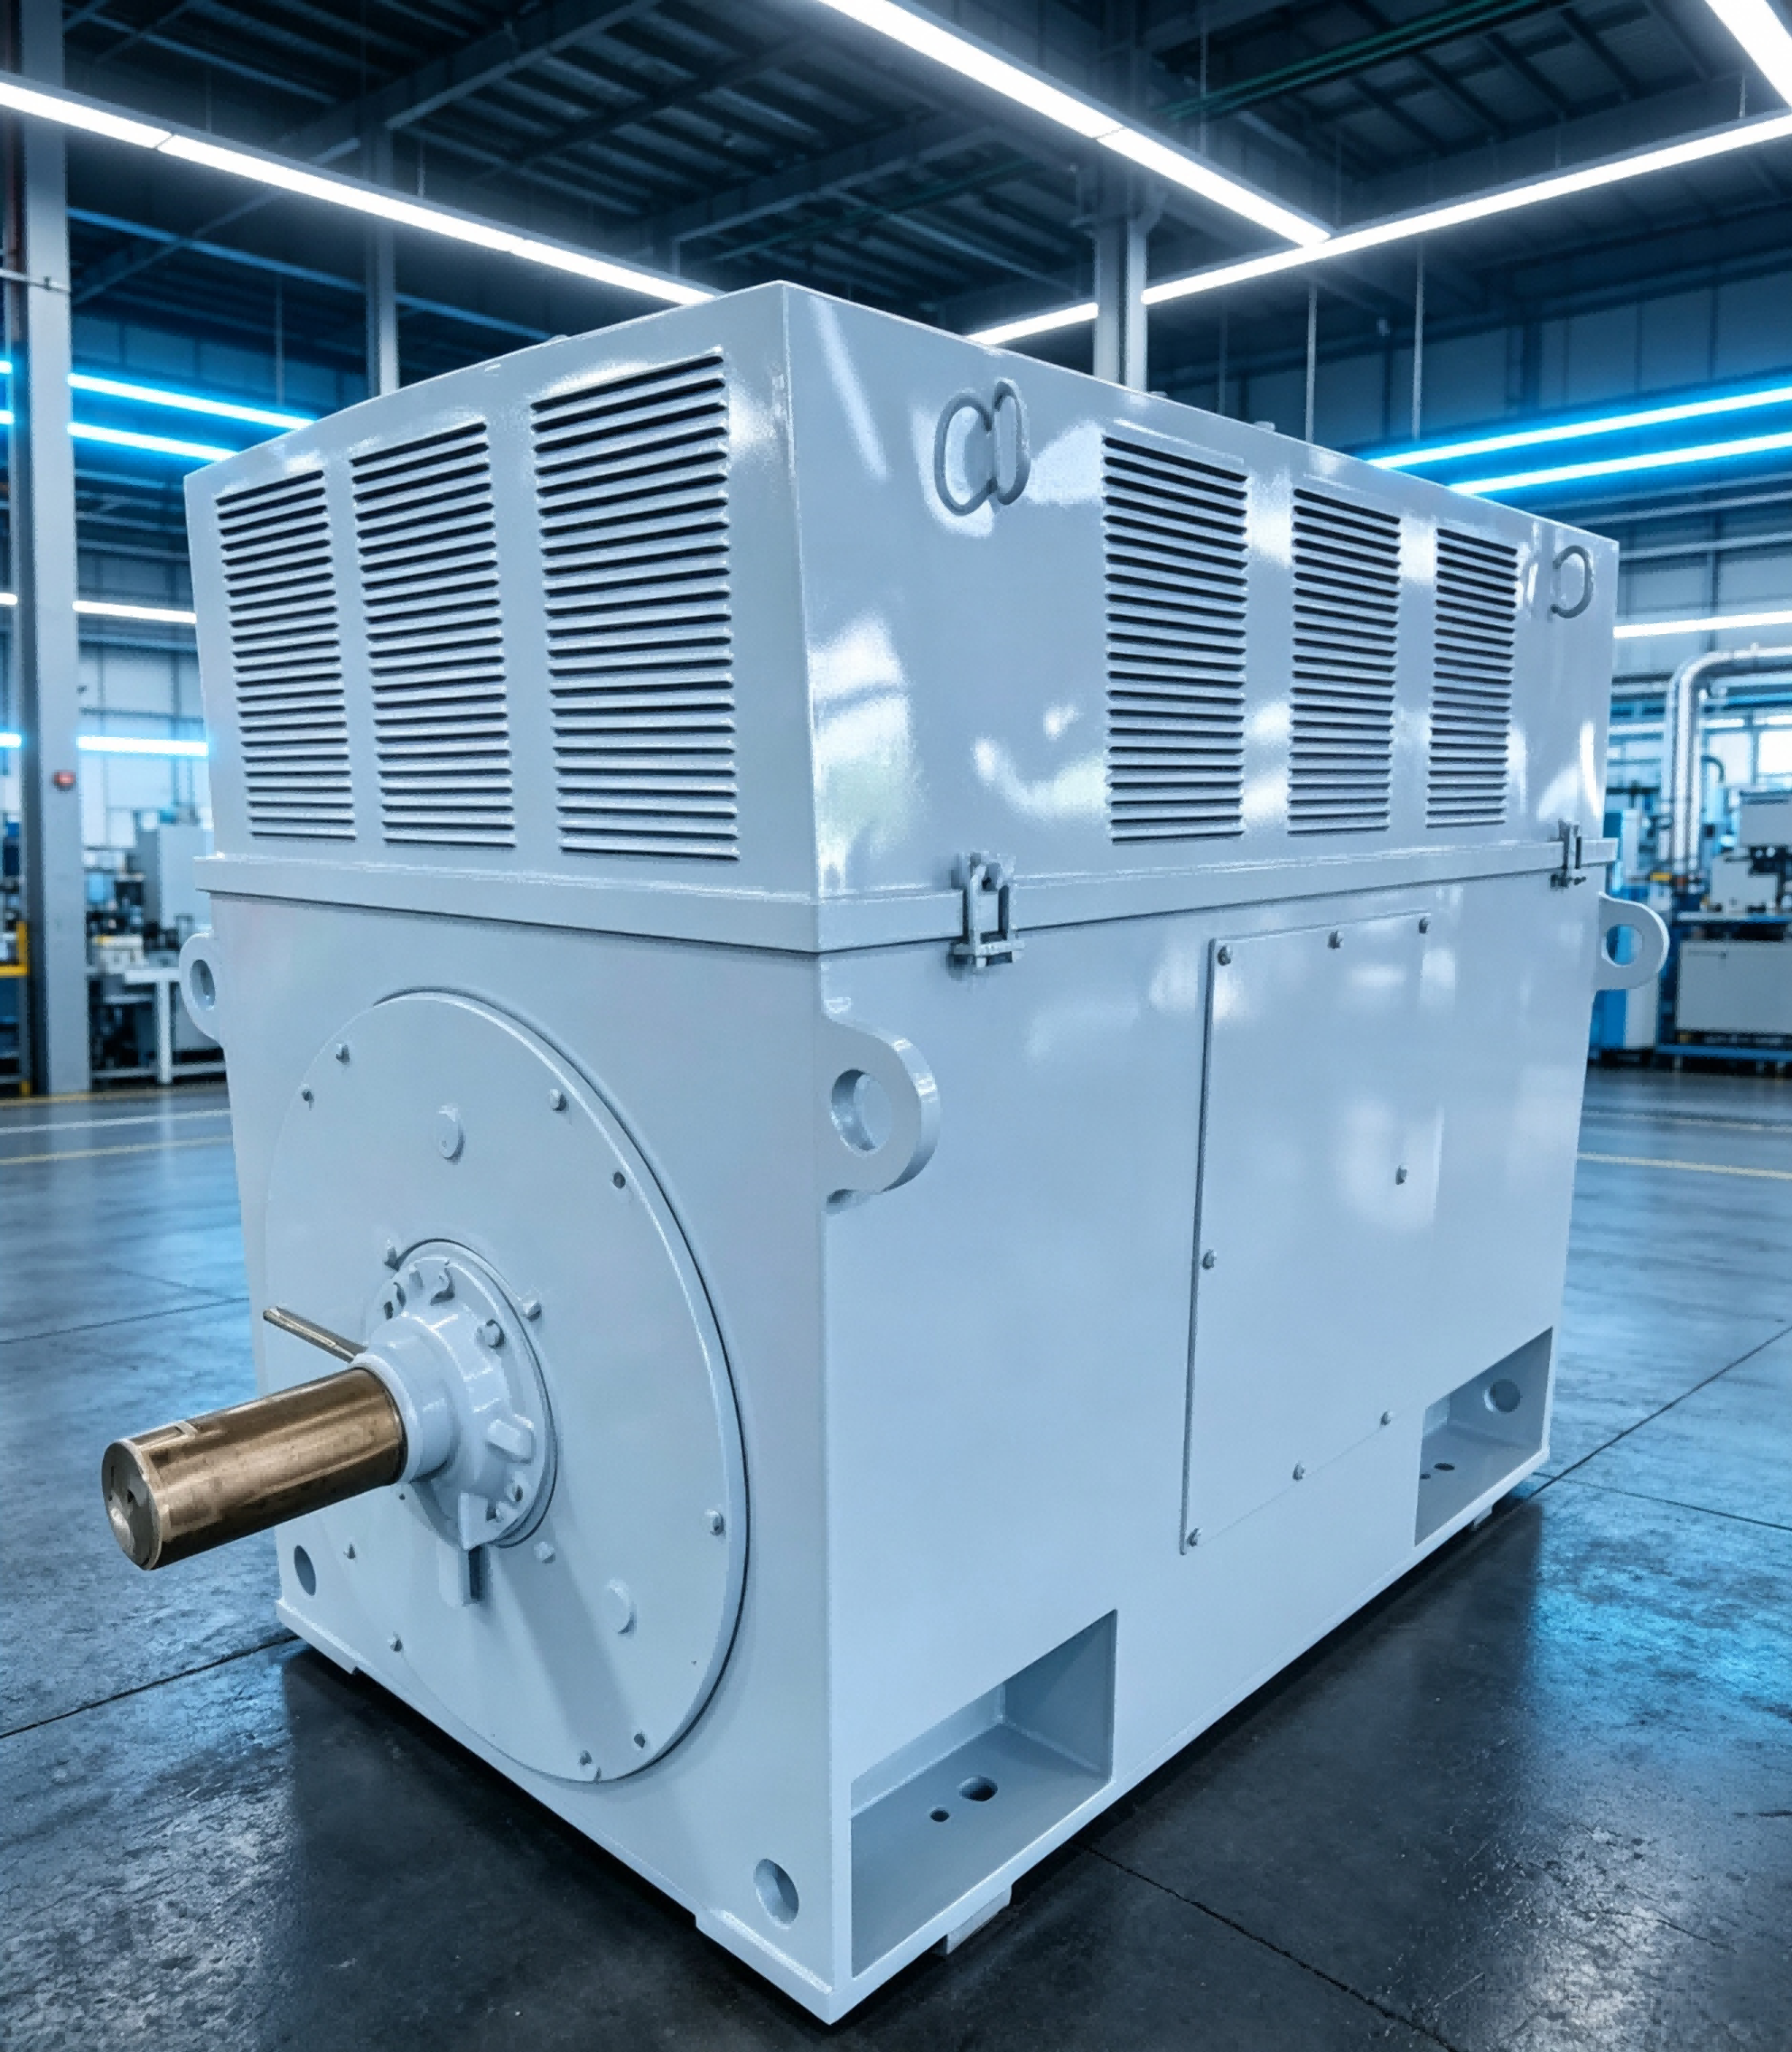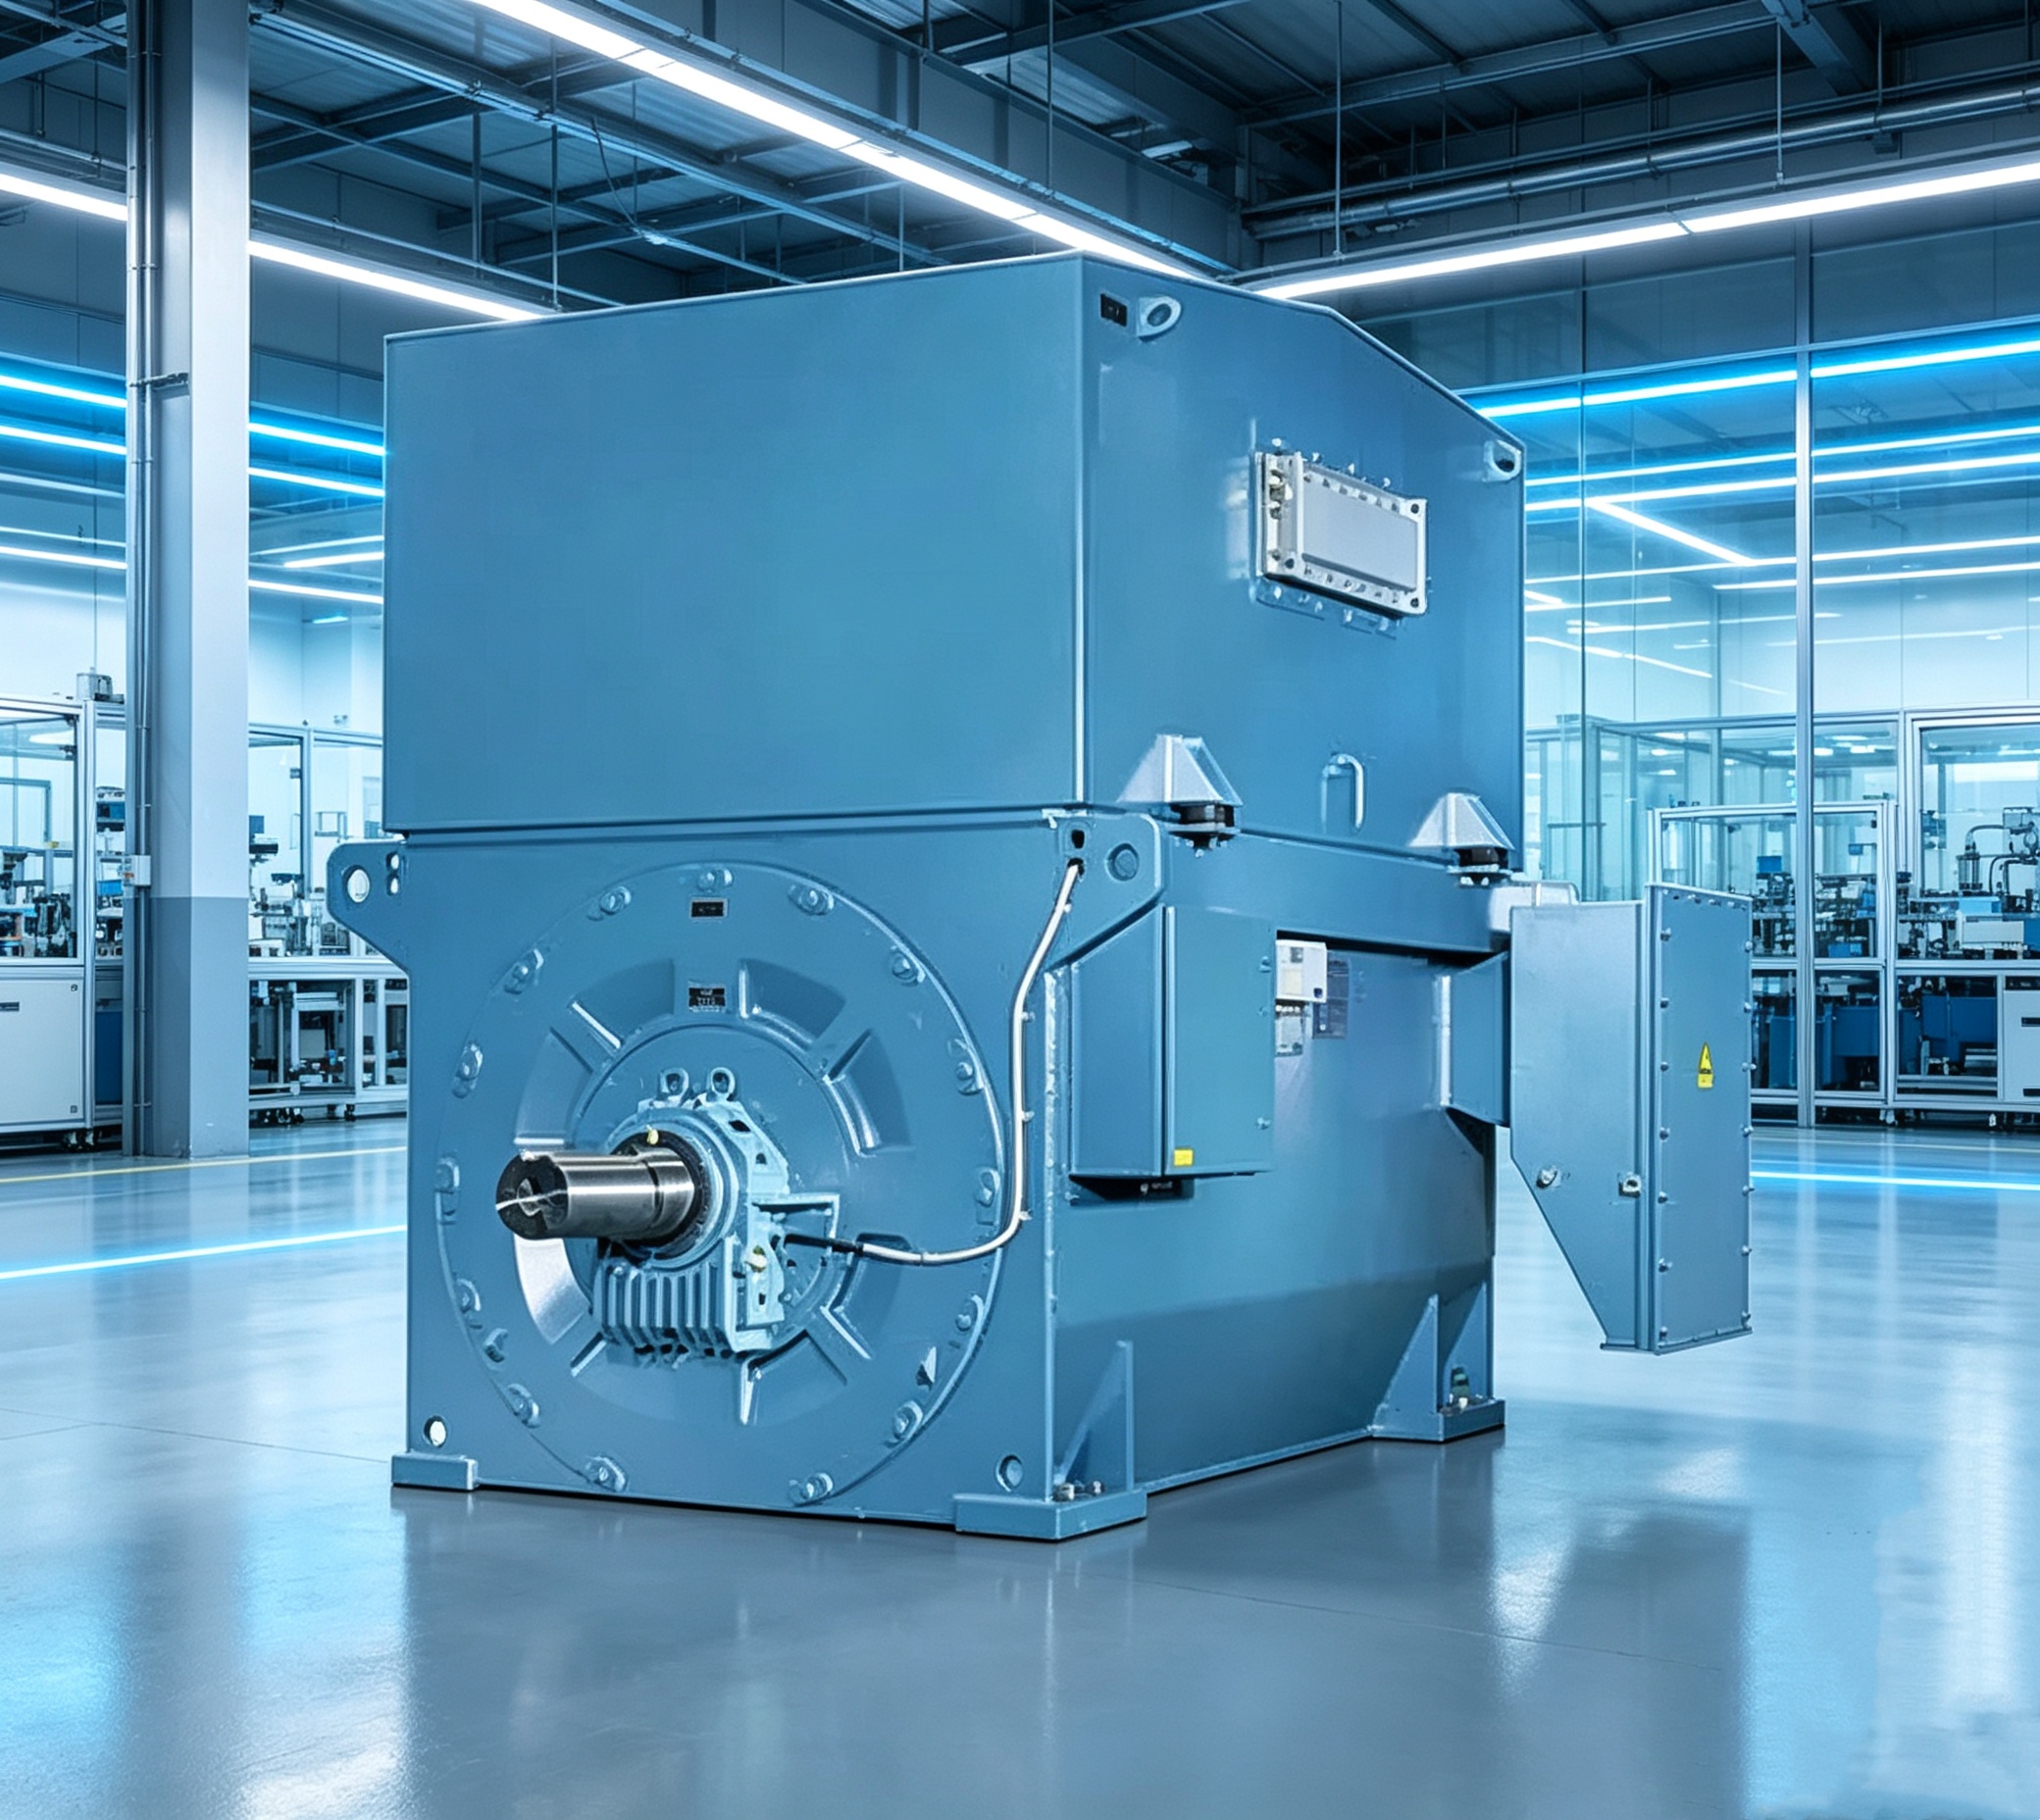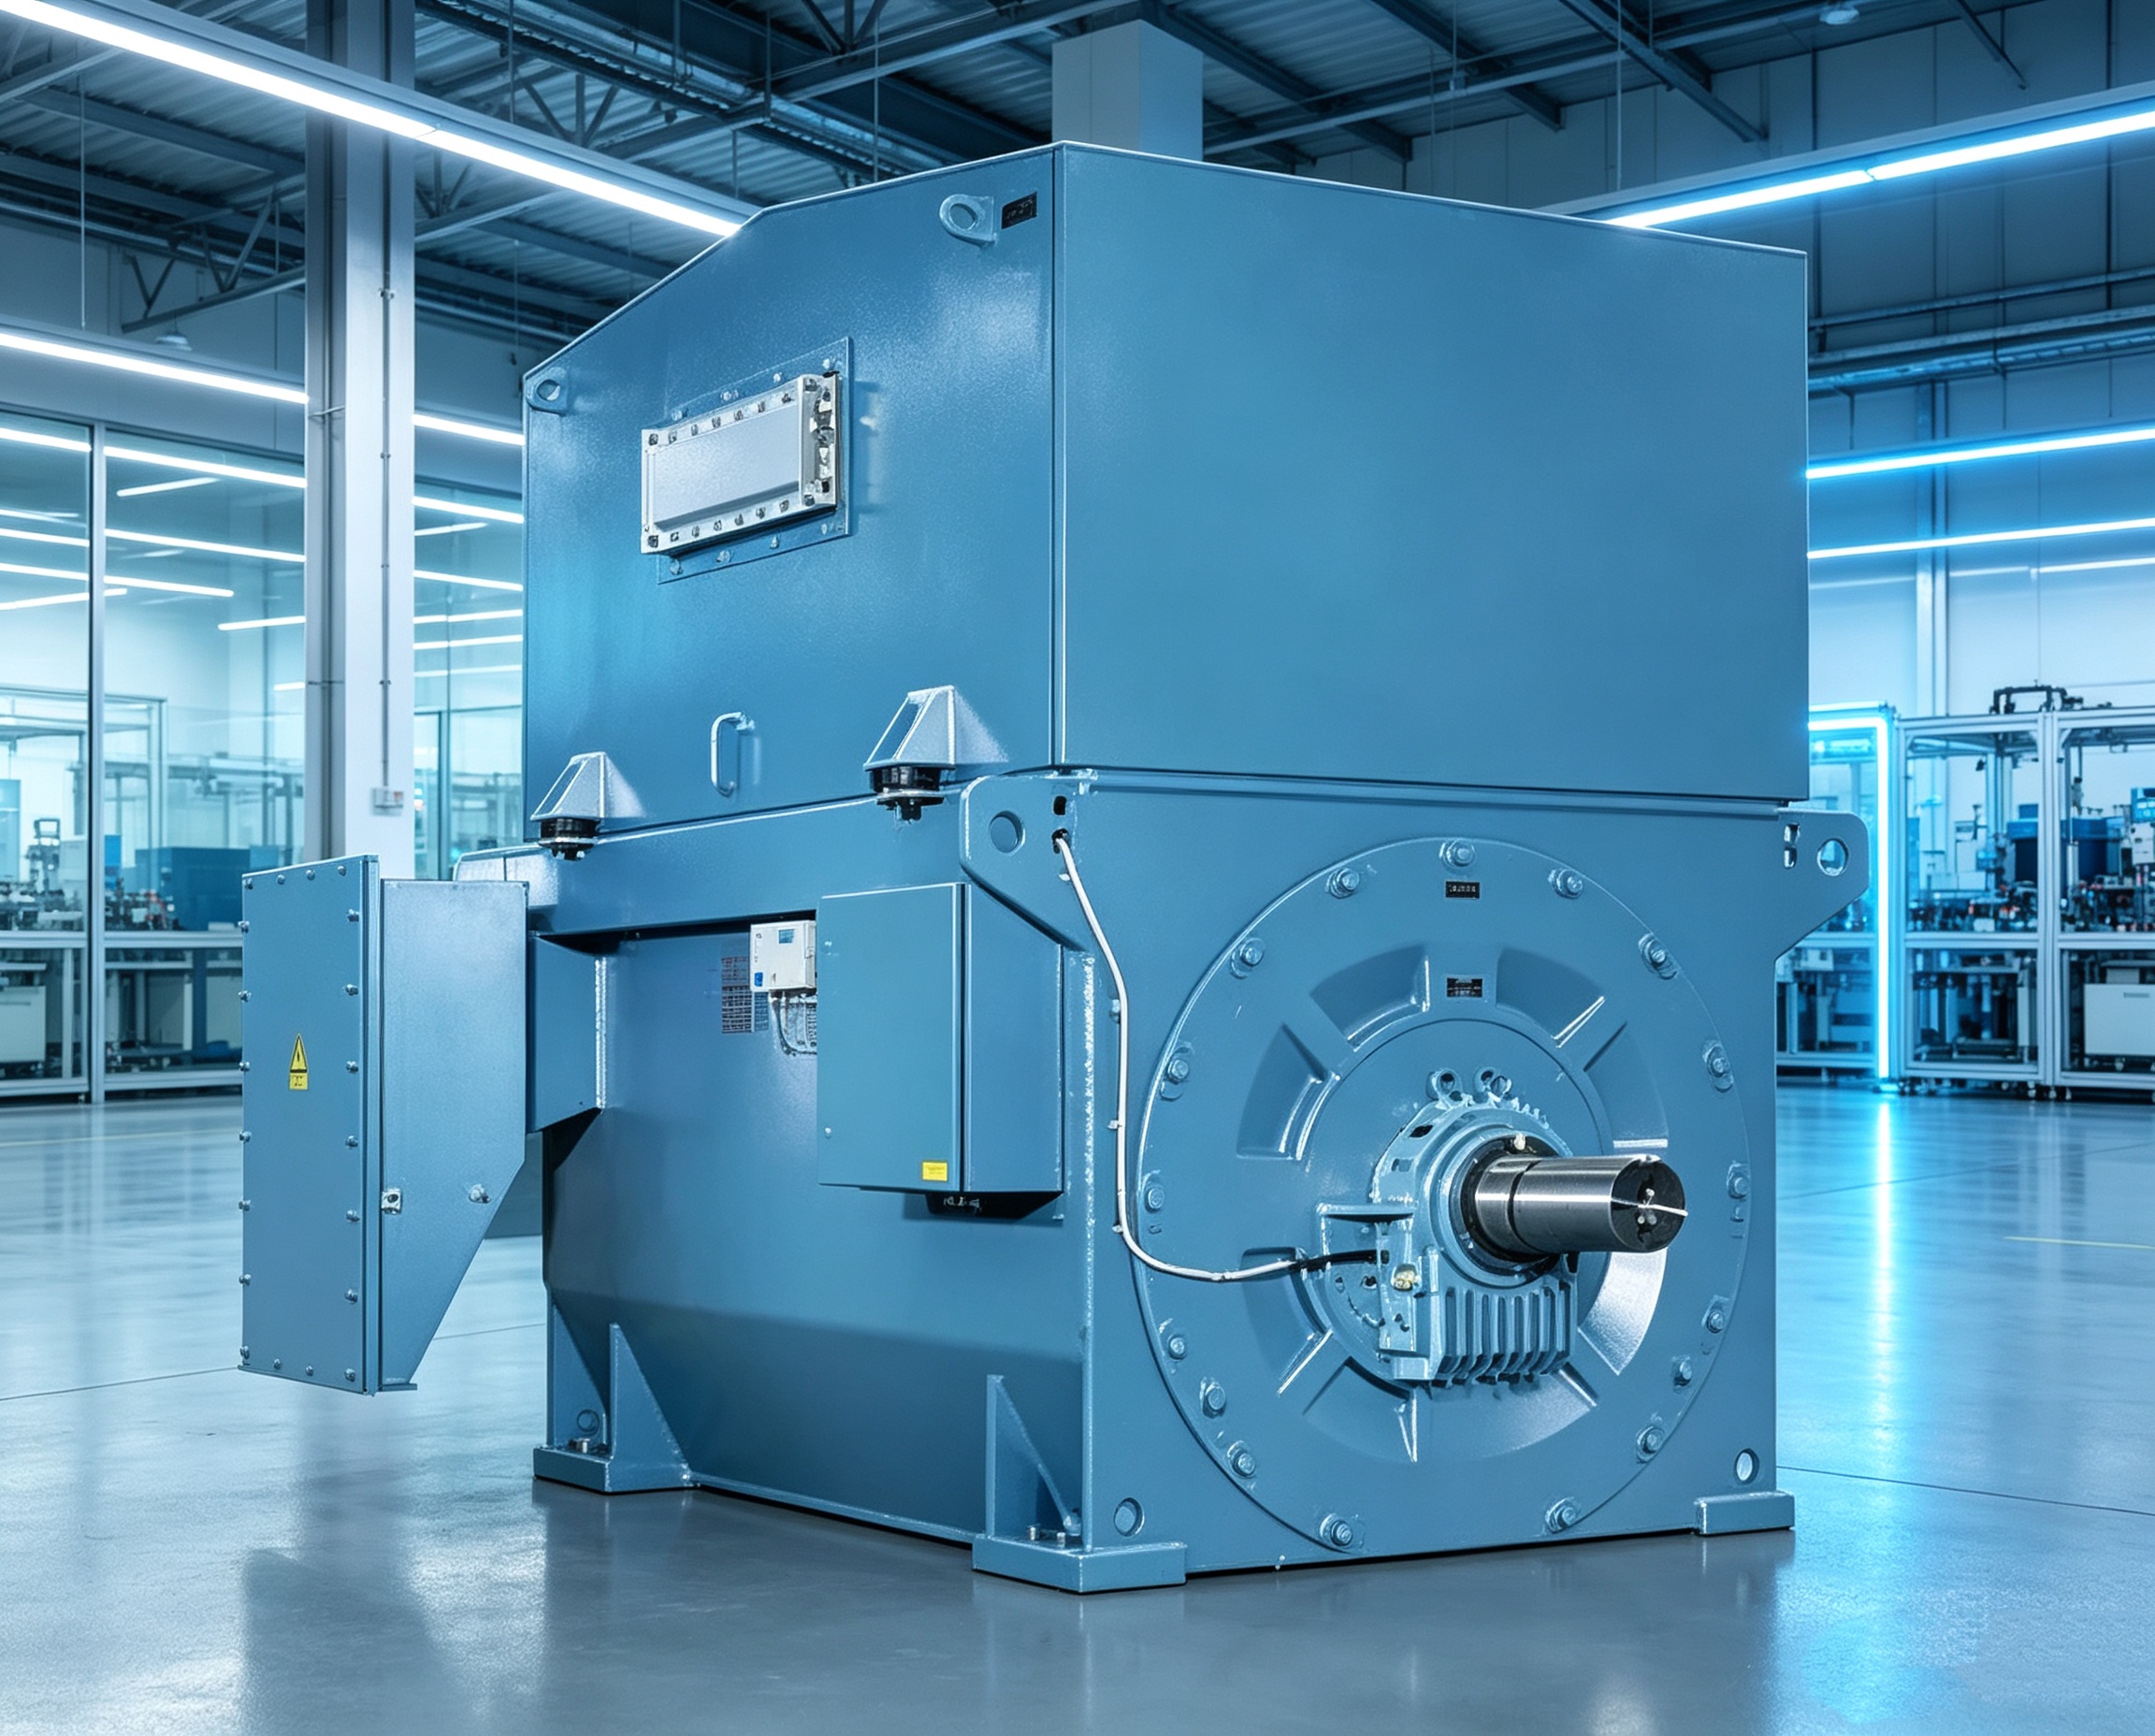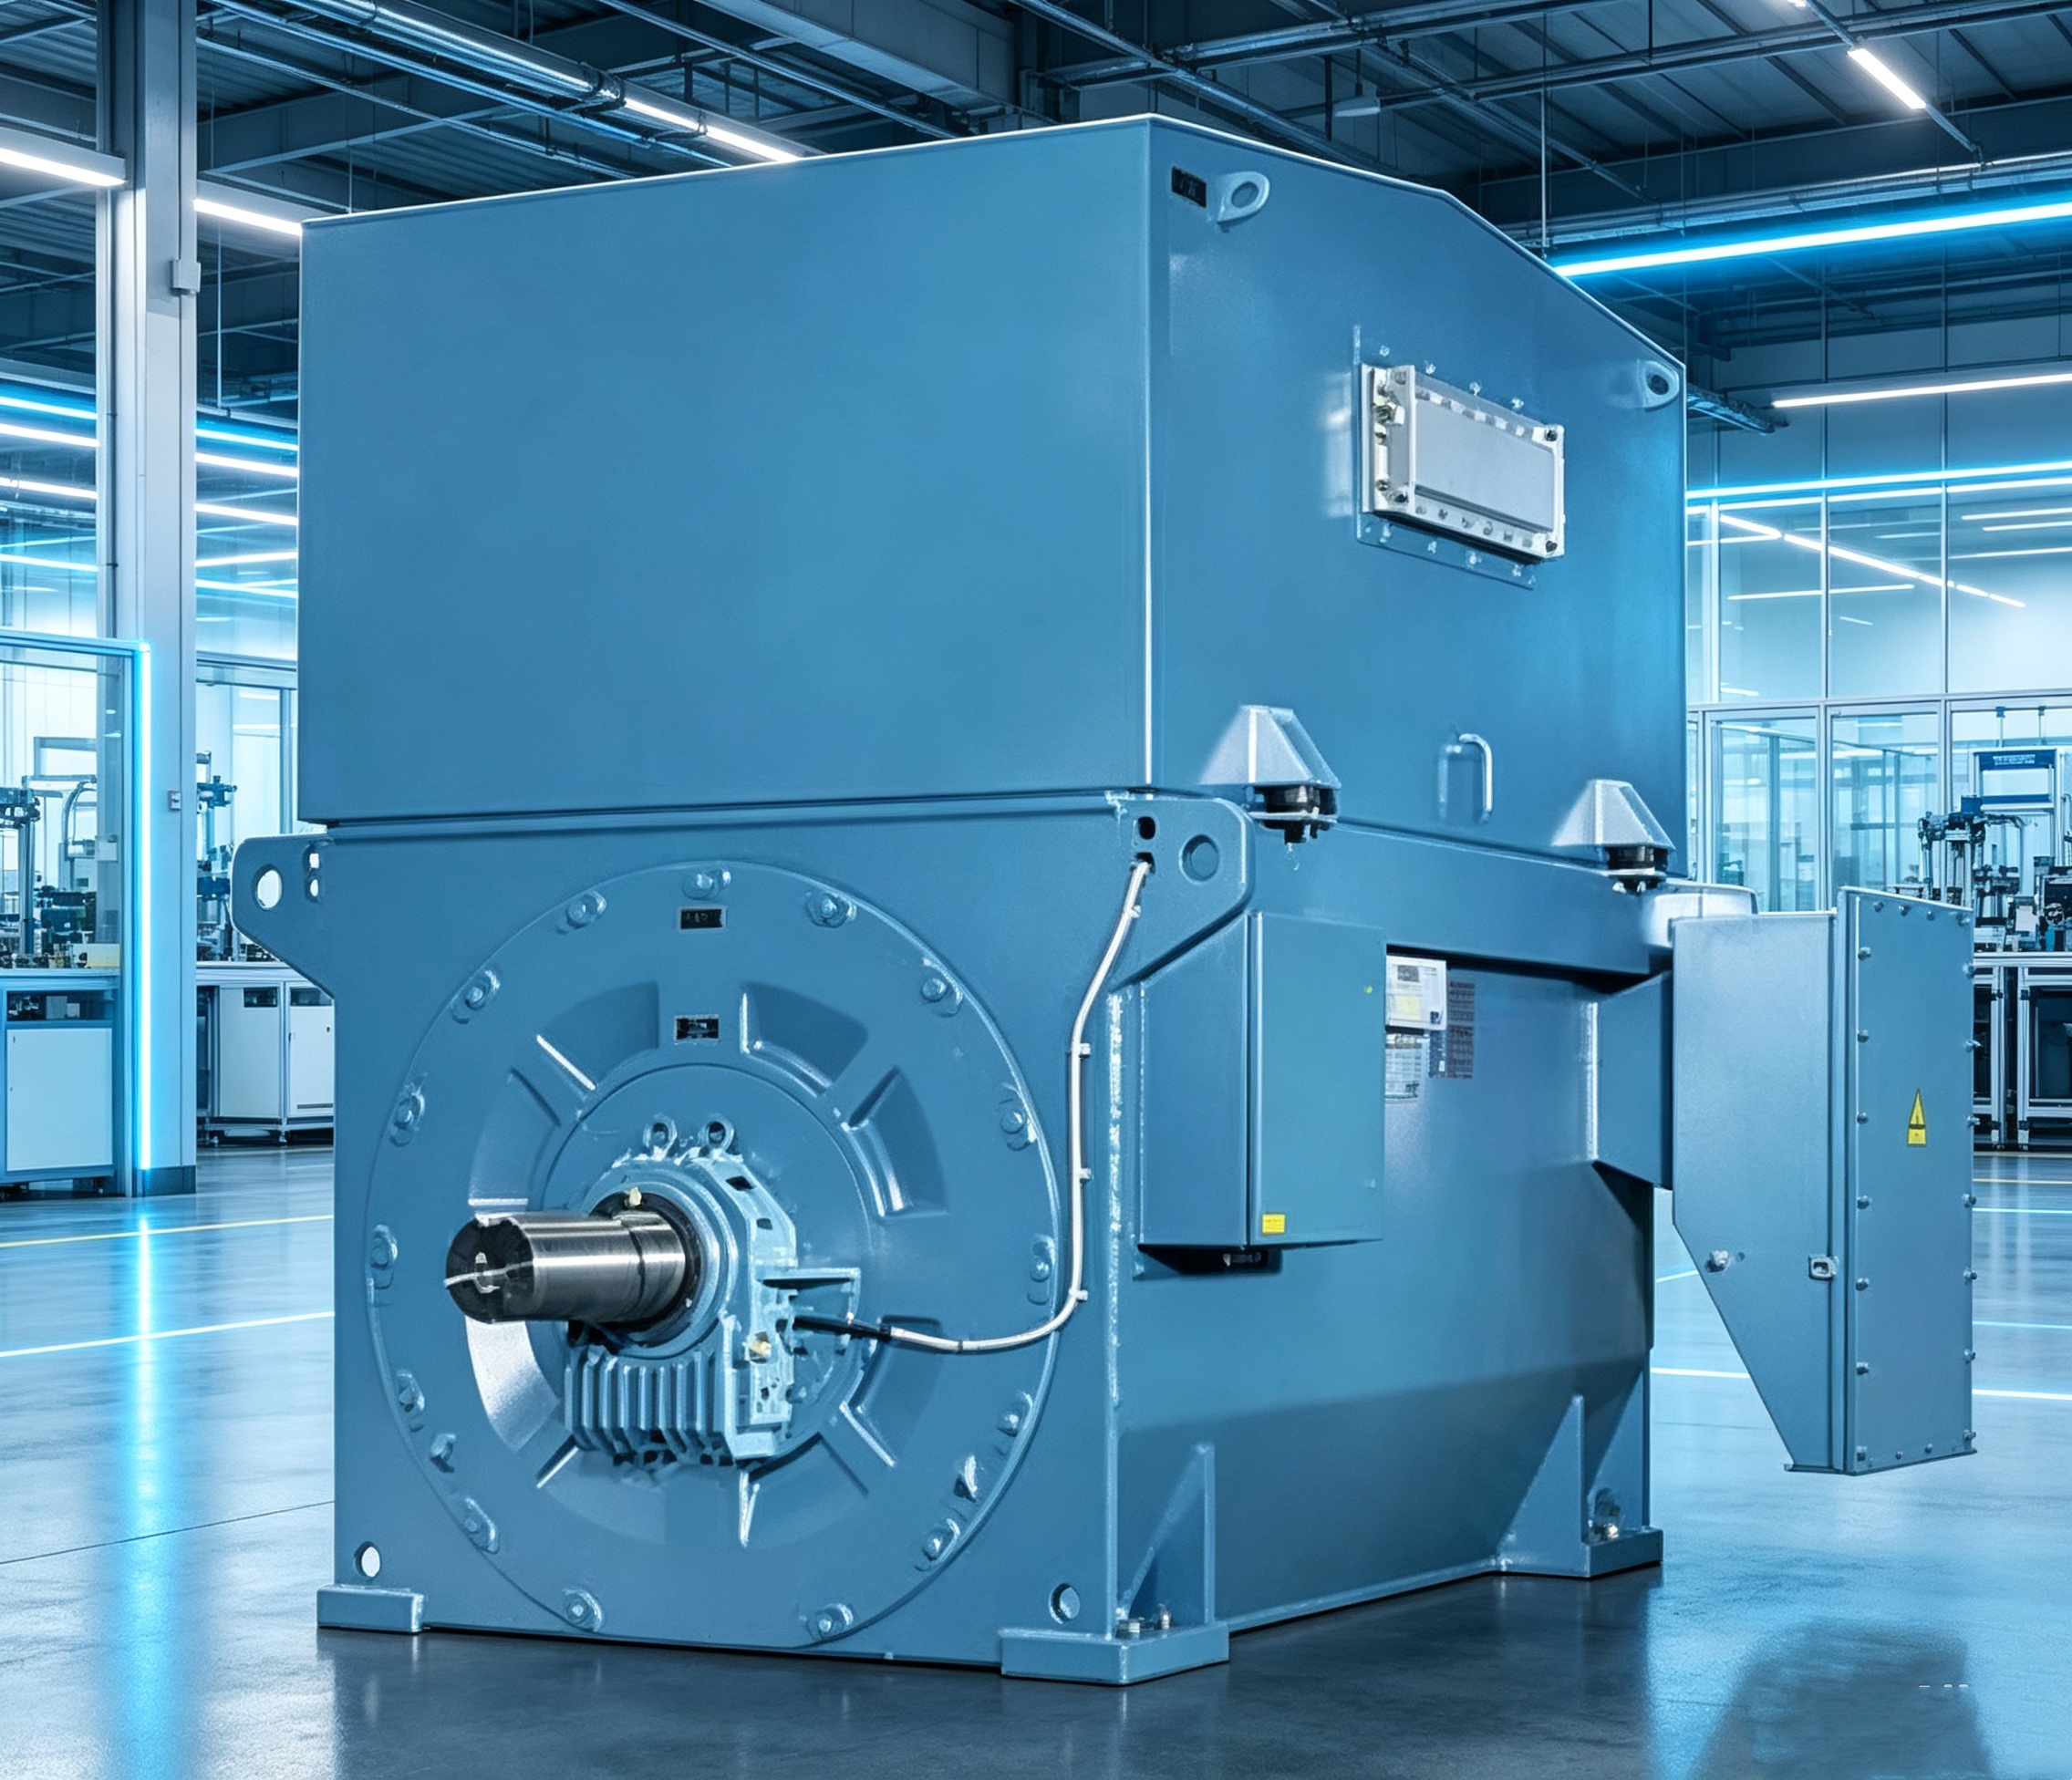
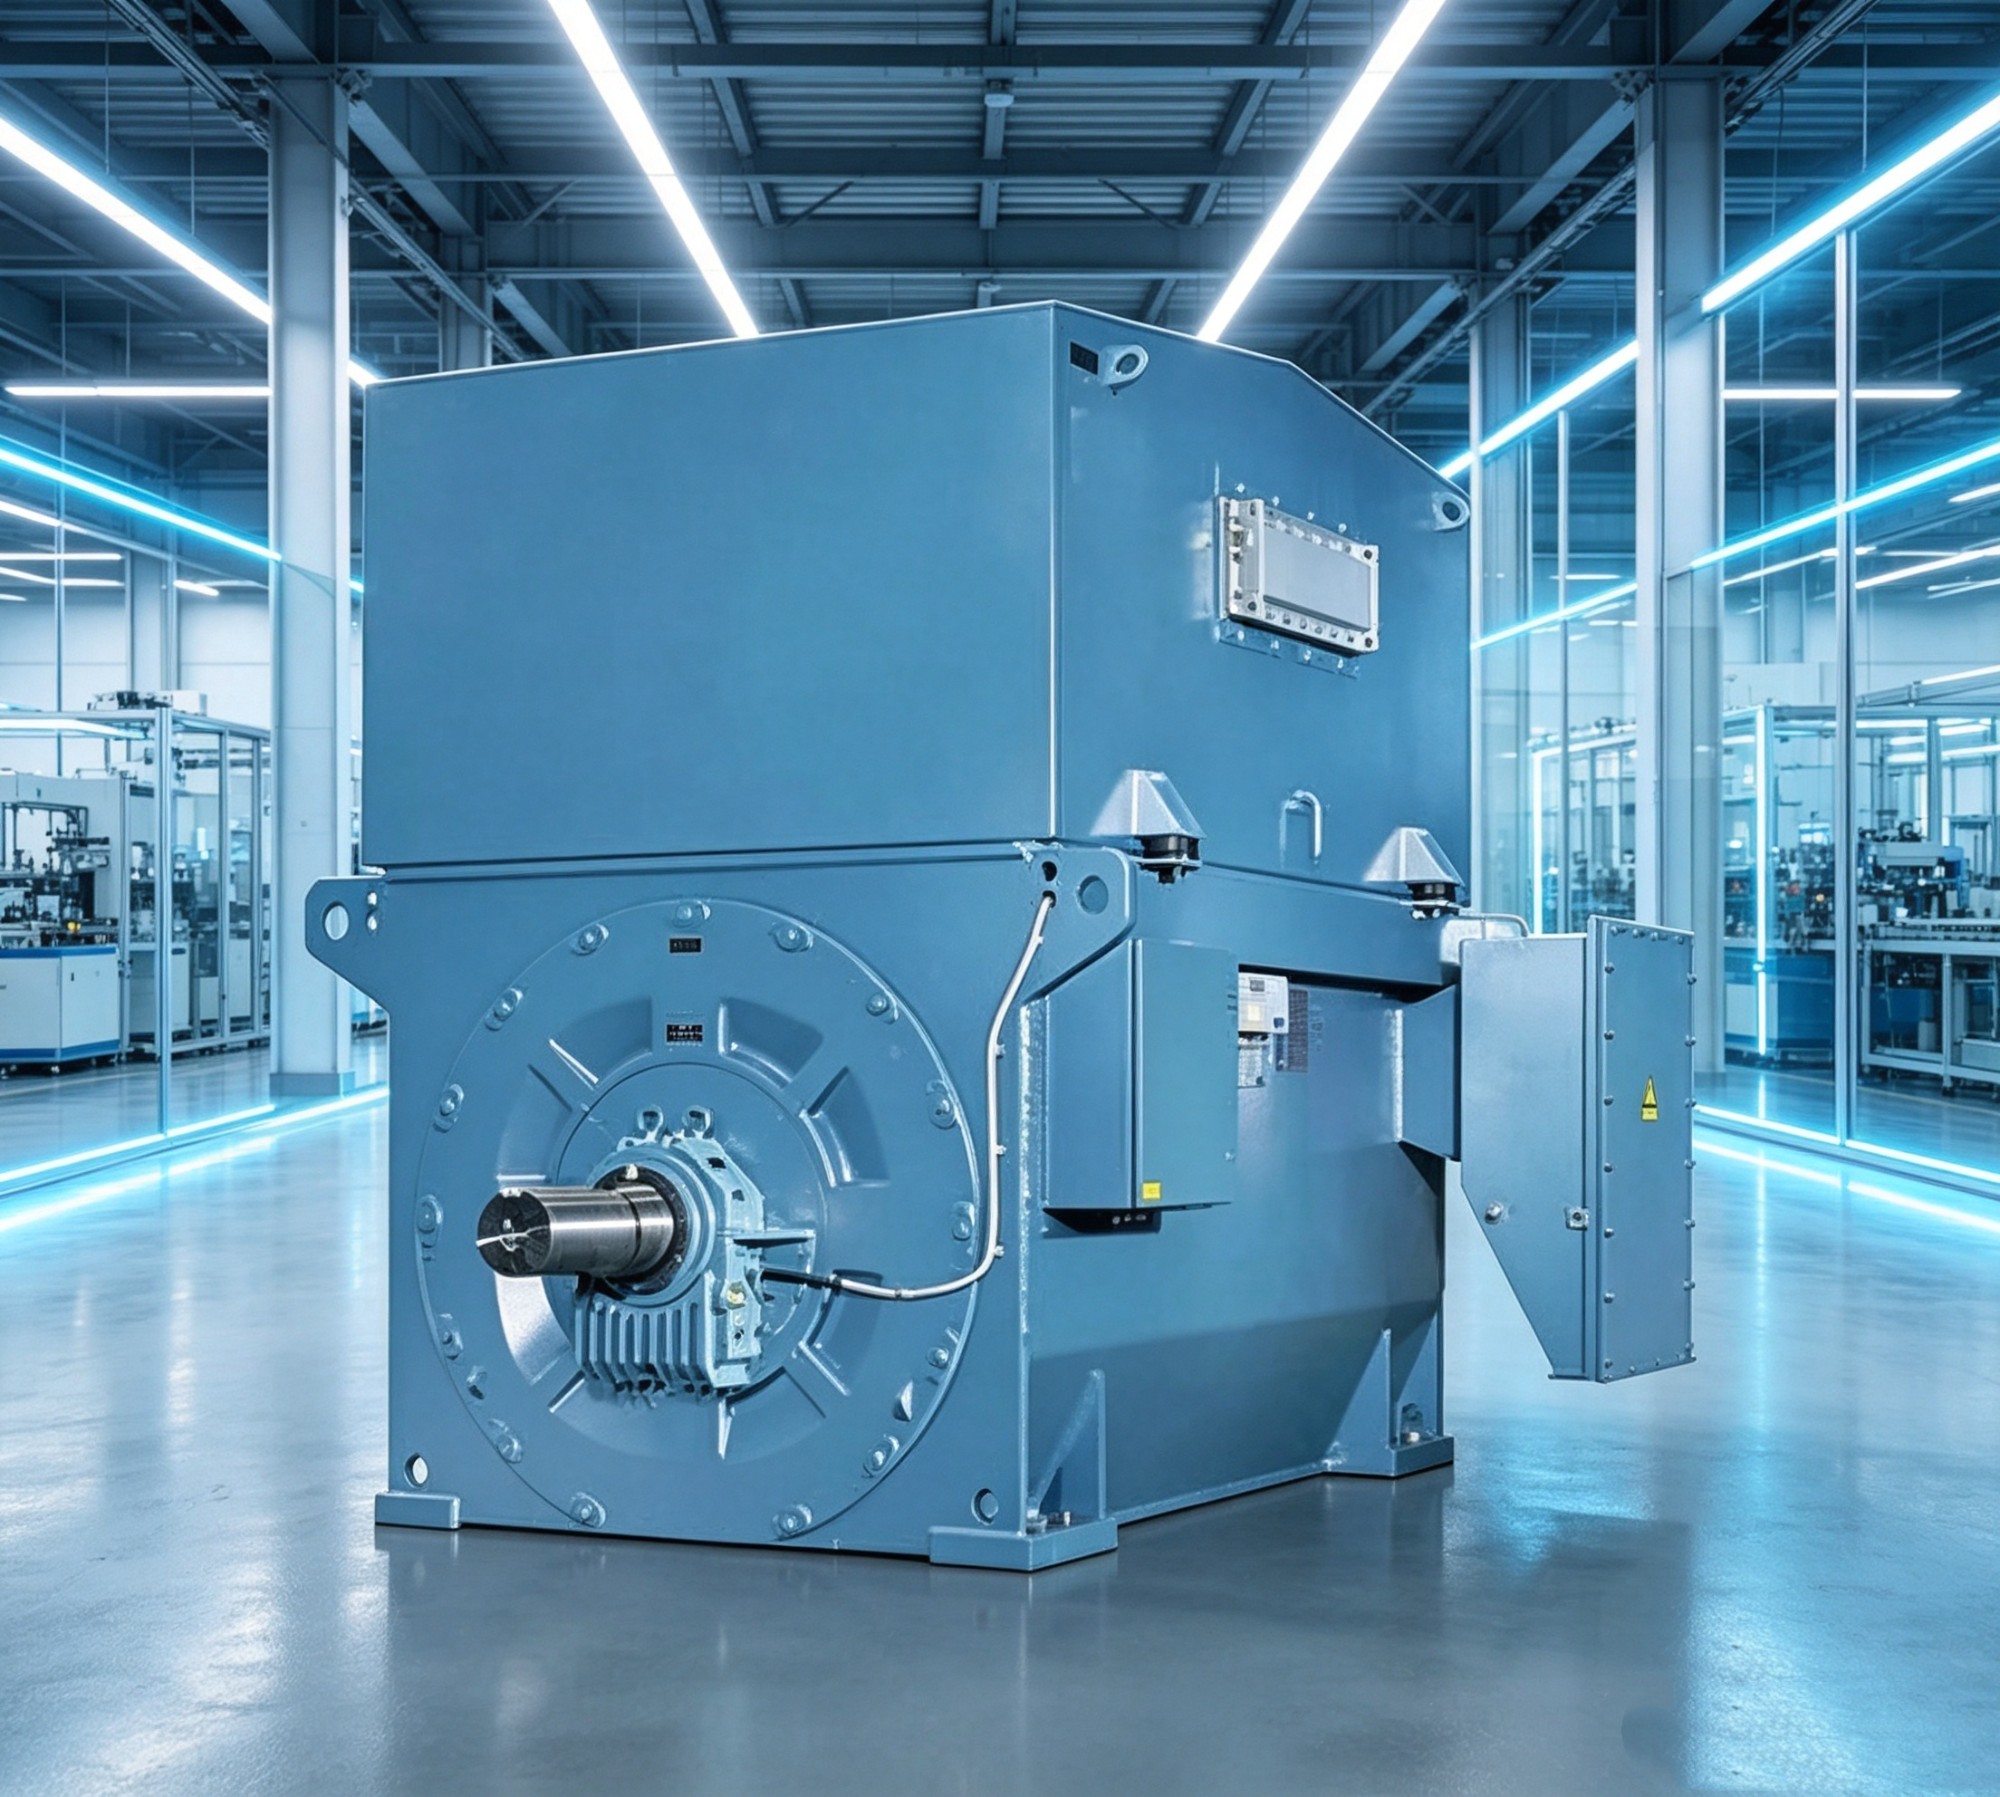
The ABB AMI 500L10A is a medium-large frame modular high-voltage squirrel-cage induction motor built on ABB’s proven AMI product platform, covering rated power from 710kW to 1100kW. Adopting a 10-pole design, it features a synchronous speed of 600rpm, with standard rated voltage of 6000V and 50Hz frequency. Designed and manufactured in accordance with IEC and NEMA international standards, this welded steel-plate motor is engineered for S1 continuous heavy-duty operation. It is normally configured with IC611 air-to-air closed cooling and IP55 protection grade. Thanks to its modular mechanical architecture, cooling assemblies, condition-monitoring sensors and auxiliary components can be flexibly configured to adapt to the dusty, high-load working conditions inside cement plants. It is specially developed to drive pumps, blowers, fans and grinding mills on cement production lines, and also widely applied in mining, water conservancy and petrochemical industries for low-speed high-torque process equipment.
| Technical Item | Specification |
|---|---|
| Model | AMI 500L10A |
| Rated Power Range | 710kW ~ 1100kW |
| Number of Poles | 10-pole |
| Synchronous Speed | 600rpm |
| Rated Voltage | 6kV standard; 3kV / 10kV optional |
| Rated Frequency | 50Hz |
| Insulation Class | Class F, temperature rise assessed at Class B |
| Protection Grade | IP55 standard; IP54 / IP56 optional |
| Cooling Method | IC611 Air-to-air closed cooling; IC81W air-to-water cooling optional |
| Rotor Type | Heavy-duty copper-bar squirrel cage |
| Frame Construction | Welded steel-plate modular frame |
| Mounting Form | IMB3 horizontal; vertical IMV1 available upon request |
| Duty Type | S1 continuous operation |
| Max Permissible Altitude | ≤1000m above sea level |
Electromagnetic performance is optimised by multi-working-point finite element simulation, tuned for the low-speed high-torque and fluctuating load characteristics of cement plant mills, blowers and pumps. It can withstand long-term continuous running and frequent load changes during cement production. The stator core is stacked with premium low-loss silicon steel laminations to minimise iron loss, stray loss and magnetic leakage under full-load and partial-load operating conditions. Stator windings adopt high-grade corona-resistant magnet wire and undergo complete VPI vacuum pressure impregnation treatment. The reinforced winding-end structure improves mechanical rigidity, dielectric strength and resistance to electrical ageing, enabling the motor to resist industrial grid voltage fluctuations and repeated starting impacts from grinding and air handling equipment. The rotor uses a heavy-duty copper-bar squirrel cage structure with strong mechanical stiffness, low rotor losses and stable starting torque. Each rotor assembly passes multi-stage high-precision dynamic balancing calibration to keep vibration and noise strictly within IEC limits, meeting the stable operation requirements of cement process machinery.
The welded modular steel-plate frame is a signature advantage of the ABB AMI series, supporting flexible matching of cooling systems and auxiliary accessories to suit dusty cement workshop environments. The AMI 500L10A is equipped with standard IC611 air-to-air closed cooling. Two independent air circuits operate inside the motor: internal hot air circulates within the sealed frame and transfers heat to external ambient air through the top-mounted air-to-air heat exchanger. The IP55 enclosure provides reliable defence against cement dust and splashing water, making it suitable for humid and dusty cement production workshops where open-ventilated motors are prone to premature failure. For sites with poor ventilation and limited heat dissipation conditions, the IC81W air-to-water cooling option can be selected to improve heat exchange efficiency.
The bearing system is customised for 10-pole low-speed heavy-load working scenarios for pumps, blowers and mills. Heavy-duty rolling bearings are standard for this frame size, while sliding bearings can be supplied for the upper power range or applications with heavy shock and vibration loads. PT100 temperature sensors can be factory-preinstalled in stator windings and bearing housings, transmitting real-time temperature data to the plant DCS system for remote condition monitoring and overtemperature protection. Space heaters are available as an option to prevent winding condensation during long standby periods of cement equipment. For variable-frequency energy-saving retrofit projects, an IC616 cooling variant can be provided to guarantee sufficient cooling airflow under low-speed variable-frequency operation. Customisation options include ATEX explosion-proof modification, high-altitude adaptation, tropical anti-humidity and anti-corrosion coating, special terminal box layout and double shaft extension to fulfil complex project specifications.
Typical driven machinery covers cement grinding mills, raw material pumps, process blowers, large exhaust fans and heavy-duty slurry pumps. The motor supports direct-on-line starting or high-voltage soft starter starting, subject to the short-circuit capacity of the on-site power grid. Before shipment, every motor undergoes comprehensive factory acceptance tests, including insulation resistance test, power-frequency withstand voltage test, no-load running test, efficiency verification, vibration and noise measurement. Built on ABB’s mature AMI modular platform, AMI 500L10A delivers stable and dependable continuous operation, convenient spare parts interchangeability and low life-cycle cost for cement production and other heavy industrial applications.